Chapter 18: Implementation - The Human Challenge |
18.1 The Software Is the Easy Part |
When a mechanical factory decides to implement an ERP system, the natural focus is on the software. Which vendorWhich modulesWhich serversThe questions are technical, and the answers seem objective. But experienced implementers know a secret. The software is the easy part. The hard part is the people. |
An ERP system is not just a set of programs. It is a new way of working. It requires people to change habits they have developed over years or decades. It requires them to trust data instead of intuition. It requires them to be disciplined about entering information that they never had to enter before. It requires them to accept that their old ways of doing things may no longer be acceptable. |
The failure rate for ERP implementations is high. Studies suggest that fifty to seventy percent of implementations fail to achieve their objectives. The causes are rarely technical. The servers work. The software runs. The failures are human. People resist change. People do not use the system as intended. People find workarounds that defeat the system's purpose. People give up when the system is difficult. |
This chapter explores the human challenge of ERP implementation. It describes why people resist, how to overcome resistance, and how to build a culture that embraces the new system. It argues that successful implementation is not about technology. It is about leadership, communication, training, and patience. |
|
18.2 Why People Resist |
Resistance to a new ERP system is not irrational. People have good reasons to resist. Understanding those reasons is the first step to overcoming them. |
Fear of incompetence is the most common reason. An experienced machinist who has been doing the job for twenty years knows how to do it well. The new ERP system requires them to learn new skills - scanning barcodes, using touchscreens, entering data. They are afraid of looking foolish. They are afraid of making mistakes. They are afraid that their hard-won expertise will be devalued. |
Loss of autonomy is another reason. In the old system, the machinist had discretion. They could decide which order to run next, based on their judgment of what was urgent. The new ERP system tells them what to run. The system, not the person, makes the decision. This feels like a loss of control. |
Fear of exposure is related. In the old system, a slow day or a small mistake could be hidden. The supervisor might not notice. The new ERP system tracks everything - start times, completion times, scrap rates, quality results. The machinist's performance is visible. This is frightening. |
Skepticism about benefits is common. People have seen many new systems come and go. They have been promised that each new system would make their jobs easier. Too often, the promise was not kept. They see the ERP as just another management fad, not worth the effort. |
Genuine inconvenience is real. The new system takes time. Scanning a barcode takes a few seconds. Entering a measurement takes a few seconds. Those seconds add up. The machinist feels that the system is slowing them down, and they are not wrong - at least not at first. |
These reasons are not excuses. They are real concerns that must be addressed. Dismissing them as laziness or stubbornness is a guarantee of failure. |
|
18.3 The Role of Leadership |
Leadership is the single most important factor in ERP implementation success. If the factory's leaders are not committed, the implementation will fail. If the leaders are committed but do not show it, the implementation will fail. Leadership must be visible, consistent, and unwavering. |
The plant manager must be the champion of the ERP. They must talk about it regularly - in meetings, in emails, in hallway conversations. They must explain why the system is important for the factory's future. They must answer questions honestly. They must celebrate successes and learn from failures. |
The plant manager must also use the system themselves. If the manager continues to use old spreadsheets and paper reports, the message to the workforce is clear: the ERP is not really important. The manager must be seen entering data, running reports, and making decisions based on the system's output. |
Middle managers - production supervisors, quality managers, maintenance supervisors - are especially important. They are the ones who will enforce the new processes. If they are not committed, their teams will not be committed. If they complain about the system, their teams will complain louder. |
Leadership also means making tough decisions. Some employees will resist no matter what. They will refuse to use the system. They will sabotage it. They will encourage others to resist. At some point, leadership must decide: these people must change, or they must leave. This is painful, but it is necessary. A single resistant employee can poison an entire department. |
|
18.4 Communication - Telling the Story |
People need to understand why the ERP is being implemented. They need a story that makes sense to them. The story must answer three questions: Why are we doing thisWhat will change for meWhat is in it for me |
The answer to 'Why are we doing this' must be honest and compelling. 'We are losing customers because we are late too often. The ERP will help us be on time.' 'We are losing money because we have too much inventory. The ERP will help us hold the right amount.' 'We are making too many defects because we use old drawings. The ERP will make sure everyone uses the current drawing.' The story must connect the ERP to real problems that employees already recognize. |
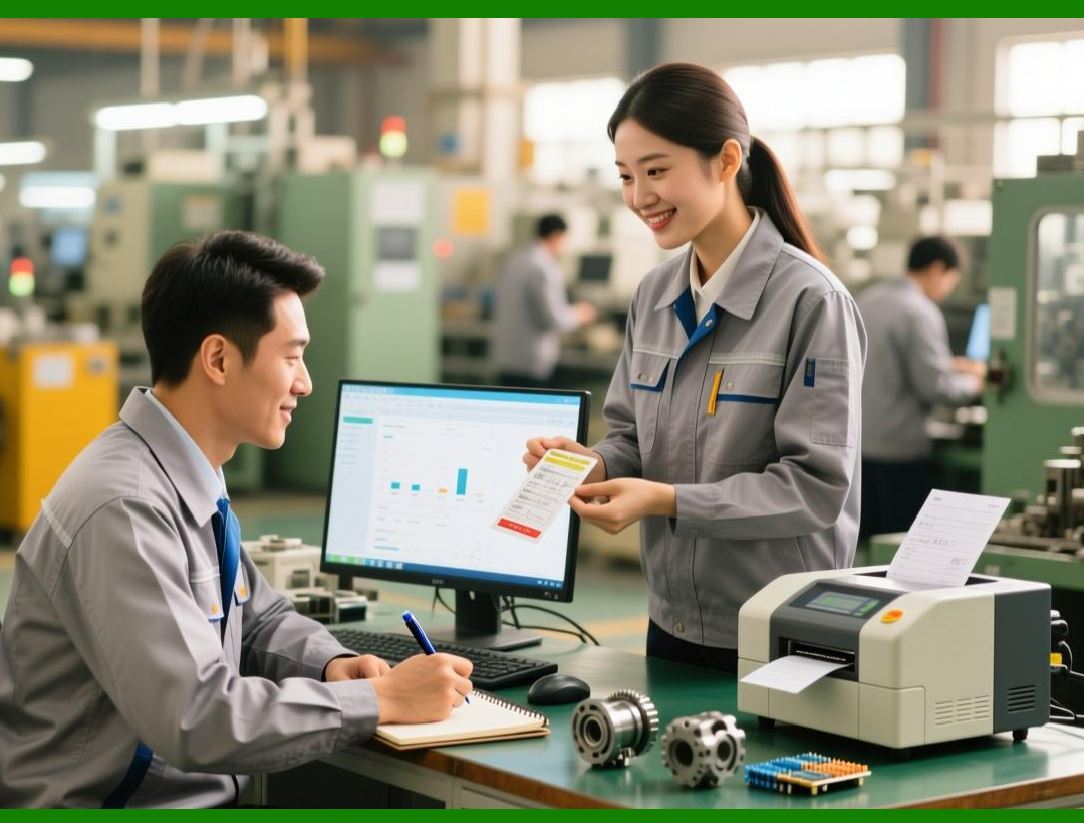
The answer to 'What will change for me' must be specific. For a machinist: 'You will have a tablet at your machine. You will scan each job when you start and when you finish. You will see the drawing on the screen. You will not have to search for paper travelers.' For a buyer: 'Purchase orders will be created automatically. You will review and approve them. You will not have to type them from scratch.' For a planner: 'MRP will calculate material requirements. You will review the action messages. You will not have to do manual calculations.' |
The answer to 'What is in it for me' must be credible. 'You will have less frustration because shortages will be fewer.' 'You will have less expediting because the schedule will be more realistic.' 'You will have more time for the parts of your job that you enjoy.' Do not promise things that cannot be delivered. Do not say 'Your job will be easier' if it will actually be harder at first. Be honest about the challenges. |
Communication must be frequent and multi-channel. Hold town hall meetings. Send emails. Post updates on bulletin boards. Have one-on-one conversations. Repeat the same messages many times, in many ways. People need to hear something seven times before it really sinks in. |
|
18.5 Training - Building Competence and Confidence |
Training is not just about teaching people how to use the software. It is about building their confidence that they can use it. A person who is afraid of the system will not use it well, no matter how much training they receive. |
Training must be role-specific. A machinist does not need to know how to create a purchase order. A buyer does not need to know how to scan a work order. Training should focus on the tasks that each person actually performs. Too much information is as bad as too little. |
Training must be hands-on. People learn by doing, not by listening. Provide practice environments where people can make mistakes without consequences. Let them enter test data, run test reports, and experience the system before it goes live. The practice environment should be as realistic as possible. |
Training must be ongoing. One day of training before go-live is not enough. Provide refresher training after a few weeks, when people have started using the system and have specific questions. Provide advanced training for power users who want to learn more. Provide new training when the system is upgraded. |
Training must be patient. Some people learn quickly. Some learn slowly. Some are comfortable with technology. Some are terrified. Adapt the pace to the learner. Use peer training - have the quick learners help the slow learners. This builds both competence and camaraderie. |
The best training is often delivered by super users - employees who have mastered the system and can help others. Identify these people early. Give them extra training. Make them available to answer questions on the shop floor. When a machinist has a problem, they want to ask another machinist, not a consultant or an IT person. |
|
18.6 The Pilot - Proving It Works |
A full-scale, factory-wide ERP implementation is risky. If something goes wrong, production stops. The better approach is to start with a pilot. Choose one product family, one department, or one shift. Implement the ERP there first. Work out the problems. Prove that it works. Then roll out to the rest of the factory. |
The pilot has several benefits. First, it limits risk. If the pilot fails, the factory can continue operating with the old system. Second, it creates a success story. When the pilot succeeds, the pilot employees become advocates. They tell their colleagues that the system works. Third, it provides a learning opportunity. The implementation team discovers what works and what does not, without affecting the whole factory. |
The pilot should be chosen carefully. Choose a product family that is representative but not too complex. Choose a department that is motivated and cooperative. Choose a shift that has strong leadership. Make sure the pilot has the resources it needs - extra training, extra support, extra patience. |
The pilot should be given a clear timeline and clear success criteria. 'By the end of the pilot, we will have on-time delivery above ninety percent for pilot products.' 'By the end of the pilot, inventory accuracy for pilot parts will be above ninety-five percent.' Measure and report progress regularly. |
When the pilot succeeds, celebrate. Recognize the pilot team publicly. Share the results with the whole factory. Use the pilot's success to build momentum for the full rollout. |
|
18.7 Managing the Go-Live |
The go-live is the moment when the factory switches from the old system to the new one. It is stressful. No matter how much preparation, something will go wrong. The key is to be ready. |
Cutover planning is essential. Decide exactly when the switch will happen - often over a weekend or a holiday. Plan every step. Who will shut down the old systemWho will migrate the dataWho will verify the migrationWho will start the new systemWho will be on call to fix problemsWrite it all down. |
Parallel running is an option. Run both the old and new systems for a period - a week, a month, a billing cycle. Enter every transaction into both systems. Compare the results. When the results match consistently, stop using the old system. Parallel running is safer, but it is also more work. People must enter every transaction twice. |
Big bang is the alternative. Switch to the new system completely, all at once. No parallel running. This is riskier, but it forces everyone to commit. There is no fallback. The factory must make the new system work. Many successful implementations use a big bang approach for its clarity and urgency. |
Whichever approach is chosen, support is critical during go-live. Have a war room staffed with experts - the implementation team, key super users, vendor consultants. Have a hotline that employees can call with problems. Have people walking the floor, answering questions, fixing issues. Be prepared for long hours. The first week after go-live is the hardest. |
|
18.8 The Post-Go-Live Dip |
After go-live, performance almost always gets worse before it gets better. This is the post-go-live dip. Orders take longer. Errors increase. People are frustrated. This is normal. It is not a sign of failure. |
The dip happens because people are learning. They are slower at first. They make mistakes. The system may have bugs. The data may have errors. The old ways are gone. The new ways are not yet fluent. Performance drops. |
The key is to manage expectations. Tell everyone ahead of time that there will be a dip. Explain that it is normal. Set a realistic timeline for recovery - often two to four weeks. Do not panic. Do not abandon the system. Do not let people go back to the old ways. |
Support the workforce during the dip. Be patient. Answer questions. Fix bugs quickly. Celebrate small victories. Recognize that people are working hard and are stressed. Do not blame. Do not punish. Do not demand perfection. |
Most implementations recover from the dip within a month. Some take longer. But the factories that persevere emerge stronger. The system begins to deliver the promised benefits. People become fluent. The dip is forgotten. |
|
18.9 The Role of Incentives |
Incentives can help drive adoption, but they must be used carefully. The wrong incentives create the wrong behaviors. |
Individual incentives - bonuses for using the system correctly - can backfire. People may focus on the incentive rather than the outcome. They may enter data that looks correct but is not. They may avoid reporting problems because problems would reduce their bonus. |
Team incentives - bonuses for the whole department achieving certain metrics - are often better. The department works together to solve problems. They help each other learn. They celebrate together. The ERP becomes a shared goal, not an individual burden. |
Recognition is a powerful incentive. A public thank-you from the plant manager. A mention in the company newsletter. A small gift card. These gestures cost little but mean a lot. People want to be appreciated. |
The most important incentive is intrinsic. People want to do good work. They want to be proud of what they produce. When the ERP helps them do better work - fewer shortages, fewer errors, less firefighting - they will adopt it willingly. The ERP must deliver on its promise. |
|
18.10 The Long Haul - Sustaining the Change |
Implementation is not an event. It is a process that takes years. The factory that succeeds in go-live can still fail later if it does not sustain the change. |
Continuous improvement is essential. The ERP is not static. The factory's processes evolve. New products are introduced. New customers are added. New challenges arise. The ERP must evolve with them. Assign someone to be responsible for the system - a full-time ERP administrator or a dedicated power user. This person keeps the system clean, updates standards, trains new employees, and solves problems. |
Regular audits are necessary. The data in the ERP will drift over time. BOMs become outdated. Routings become inaccurate. Inventory counts become wrong. Schedule regular audits - monthly for critical data, quarterly for everything else. Find and fix errors before they cause problems. |
Refresher training is needed. People forget. New employees join. The system is upgraded. Schedule regular training sessions. Keep the training materials updated. Make training an ongoing part of the job. |
Leadership attention must continue. The plant manager cannot declare victory and move on. They must continue to talk about the ERP, use the ERP, and hold people accountable for using the ERP. If the leader stops paying attention, the organization will revert. |
|
18.11 Real-World Example: The Hydraulics Manufacturer's Turnaround |
Consider a manufacturer of hydraulic cylinders. The company had attempted to implement an ERP system two years earlier. The implementation failed. The software was installed, but people did not use it. They continued to use spreadsheets and paper. The data in the ERP was inaccurate. The plant manager declared the project a waste of money. |
A new plant manager was hired. She decided to try again. She knew that the software was not the problem. The people were the problem. She started with leadership. She attended every training session. She used the ERP for her own work. She refused to look at spreadsheets. When someone brought her a paper report, she said, 'Show me in the system.' |
She communicated constantly. She held weekly town halls. She explained why the ERP was important for the factory's survival. She shared data - on-time delivery, inventory turns, scrap rates - and showed how the ERP was helping to improve them. |
She empowered super users. She identified five employees who were enthusiastic about the system. She gave them extra training and released them from some of their regular duties. They became the go-to people for questions. They walked the floor, helping others. |
She managed the go-live carefully. She chose a pilot in one product family. The pilot succeeded. She used the pilot's success to build momentum. She rolled out to the rest of the factory gradually, one department at a time. |
When the post-go-live dip came, she did not panic. She expected it. She supported her team. She fixed bugs quickly. She celebrated small wins. Within six weeks, performance had recovered and was improving. |
Today, the factory uses the ERP for everything. On-time delivery is up. Inventory is down. Scrap is down. The plant manager says the key was not the software. The key was the people. |
|
18.12 The Human Factor - Empathy and Respect |
At the heart of every successful ERP implementation is empathy. The people on the shop floor are not obstacles. They are not lazy. They are not stupid. They are human. They have fears. They have habits. They have pride. They need to be treated with respect. |
Listen to their concerns. Take them seriously. When a machinist says the tablet is too far from the machine, move it. When a buyer says the purchase order screen is confusing, simplify it. When a planner says the MRP action messages are not helpful, improve them. The system should serve the people, not the other way around. |
Involve people in the design. Ask them how the system should work. Let them test prototypes. Let them suggest improvements. When people feel ownership of the system, they will use it. When the system is imposed on them, they will resist. |
Be patient. Change takes time. Some people will adopt quickly. Some will adopt slowly. Some will never fully adopt, but they can still be productive if the system is designed well and supported well. Do not expect perfection. Expect progress. |
|
18.13 Summary: Technology Enables, People Deliver |
An ERP system is a powerful tool. It can calculate material requirements, schedule production, track inventory, manage quality, and integrate finance. But a tool is only useful if people use it. A hammer on a shelf does not drive nails. An ERP that is not used does not improve the factory. |
The human challenge of ERP implementation is not a distraction from the real work. It is the real work. Choosing the software is easy. Installing the servers is easy. Changing how people work is hard. It requires leadership, communication, training, patience, and empathy. It requires recognizing that people have fears and respecting those fears. It requires celebrating successes and learning from failures. |
The factories that succeed are not the ones with the most expensive software or the most powerful servers. They are the ones with the most committed leaders, the most engaged employees, and the most supportive culture. The technology enables. The people deliver. |
In the next chapter, we will explore how small shops can benefit from ERP, even with limited resources. The principles of implementation are the same, but the tactics differ. Small shops have advantages that large factories lack - and disadvantages that they must overcome. |
|
Key takeaways from Chapter 18: |
1. Software is the easy part - the hard part is changing how people work and overcoming resistance. |
2. People resist for valid reasons: fear of incompetence, loss of autonomy, fear of exposure, skepticism, and genuine inconvenience. |
3. Leadership is the single most important factor - leaders must be visible, consistent, and unwavering in their commitment. |
4. Communication must answer three questions: why are we doing this, what will change for me, and what is in it for me |
5. Training must be role-specific, hands-on, ongoing, and patient - it builds both competence and confidence. |
6. Super users - employees who master the system and help others - are the most effective trainers. |
7. A pilot implementation limits risk, creates a success story, and provides learning before full rollout. |
8. Go-live requires careful cutover planning, strong support, and realistic expectations of a post-go-live dip. |
9. The post-go-live dip is normal - performance drops before it improves; expect it and do not panic. |
10. Incentives can help, but recognition and intrinsic motivation are more powerful than individual bonuses. |
11. Sustaining the change requires continuous improvement, regular audits, refresher training, and ongoing leadership attention. |
12. Real-world examples show that failed implementations can be turned around with the right human approach. |
13. Empathy and respect are essential - listen to concerns, involve people in design, and treat them as partners, not obstacles. |
14. Technology enables, but people deliver - the best ERP is worthless if people do not use it. |
 cs@easiersoft.com