Chapter 6: Capacity vs. Load - Stopping Bottlenecks |
6.1 The Silent Killer of Delivery Dates |
Every mechanical factory has one. It might be a five-axis machining center that cost half a million dollars. It might be an aging but reliable heat treatment furnace that no one has bothered to replace. It might be the only inspection station with a certain type of coordinate measuring machine. Whatever form it takes, every factory has a resource that limits the entire operation. This is the bottleneck. |
The bottleneck is not just an inconvenience. It is the silent killer of delivery dates. No matter how fast the other machines run, no matter how much raw material you pile up at the receiving dock, the bottleneck determines how much finished product the factory can produce. A bottleneck that is overloaded pushes every promise later. A bottleneck that is underloaded means the factory is wasting capacity that could generate revenue. |
Before we go further, let us be very clear about terms. Capacity is the maximum amount of work a resource can do in a given period. A CNC lathe might have a capacity of eighty hours per week, assuming two shifts per day, five days per week. Load is the amount of work that has been assigned to that resource. If the MPS and MRP have scheduled one hundred hours of work on that lathe for next week, the load is one hundred hours. When load exceeds capacity, you have a problem. |
The ERP system's job is not to magically create more capacity. It cannot. The ERP's job is to make the bottleneck visible, to calculate the consequences of overloads, and to help the planner find the least painful way to bring load back into balance with capacity. This chapter explores how ERP systems perform this essential function through capacity planning tools, and how mechanical manufacturers can stop their bottlenecks from stopping their business. |
|
6.2 Why Capacity Planning Is Not Optional |
A factory that plans materials but ignores capacity is like a general who plans troop movements but ignores the terrain. The plan might look beautiful on paper, but it will fail in execution. MRP, as we saw in Chapter 5, assumes infinite capacity. It will happily schedule a hundred hours of work on a machine that only has eighty hours available. The MRP outputs are mathematically correct but practically impossible. |
What happens when the factory tries to execute an impossible planThe first sign is usually a pile of work-in-progress in front of the bottleneck machine. The upstream machines run at full speed, feeding parts into the bottleneck faster than it can process them. The work-in-progress grows. Lead times stretch. Downstream machines starve because the bottleneck is not delivering parts quickly enough. The entire factory becomes unbalanced. |
The planner reacts by expediting. They move urgent orders ahead of less urgent ones. This helps the urgent orders but delays the others. The expediting creates chaos. Workers are constantly interrupted. Setup times increase because machines are switching between jobs more frequently. Quality suffers because of the rushed pace. |
All of this is preventable with proper capacity planning. Capacity planning does not need to be perfect. It does not need to predict the future with certainty. It only needs to be good enough to identify the major mismatches between load and capacity before they cause crises. A simple warning that the heat treatment furnace is overloaded by twenty hours in week nine gives the planner time to act. They can subcontract some work, move some orders to earlier or later weeks, or authorize overtime. Without the warning, the problem is discovered when the furnace is already backed up and orders are already late. |
|
6.3 The Two Levels of Capacity Planning |
ERP systems typically offer two levels of capacity planning, corresponding to different levels of detail and different time horizons. The first level is Rough-Cut Capacity Planning (RCCP) , which we introduced briefly in Chapter 4. RCCP works at the level of the Master Production Schedule. It uses simplified routings that only include the critical bottleneck resources. For each product family, the planner enters approximate hours per unit on each critical resource. Then RCCP applies the MPS to those simplified routings and produces a weekly or monthly view of load versus capacity. |
RCCP is fast and high-level. It can run in seconds and give a manager a clear picture of whether the MPS is feasible. If RCCP shows no overloads, the MPS is probably feasible. If RCCP shows significant overloads, the MPS needs adjustment before the factory commits to detailed material planning. |
The second level is Capacity Requirements Planning (CRP) . CRP works at the level of individual work orders, after MRP has been run and firm orders have been released. CRP uses the full routing for each order, including every operation, every setup time, and every run time. It schedules each operation on each work center, respecting the order's due date and any precedence constraints. CRP produces a detailed, time-phased view of load on every work center, often in daily or even hourly buckets. |
CRP is detailed and accurate, but it is computationally intensive and depends on firm order data. If the schedule changes frequently, CRP becomes outdated quickly. Most mechanical factories use RCCP for medium-term planning and use a simplified version of CRP for short-term scheduling. The ERP system supports both, and the planner chooses the right tool for the planning horizon. |
|
6.4 The Theory of Constraints - Finding the Real Bottleneck |
In the 1980s, a physicist named Eliyahu Goldratt wrote a novel called 'The Goal' that changed how manufacturing people think about capacity. Goldratt argued that most factories waste enormous effort optimizing non-bottleneck resources, while ignoring the one or two resources that truly limit output. His Theory of Constraints (TOC) provides a simple, powerful framework: identify the bottleneck, exploit it, subordinate everything else to it, elevate it, and then repeat the cycle. |
The ERP system is an ideal tool for implementing TOC. The first step is to identify the bottleneck. In a small factory, the bottleneck might be obvious - a slow machine that everyone complains about. In a large factory, the bottleneck might move depending on the product mix. The ERP can help by analyzing historical data. Which work center consistently has the highest utilizationWhich work center is always the one with orders waiting in front of itWhich work center's downtime correlates most strongly with late deliveriesThe answers point to the bottleneck. |
Once the bottleneck is identified, the ERP helps to exploit it. Exploitation means ensuring that the bottleneck never wastes a minute. It should never be idle because of a missing tool, a missing program, or a missing operator. It should never be processing parts that are not needed for current customer orders. The ERP can schedule the bottleneck first, filling its capacity with the most urgent and profitable work. Then the ERP schedules the non-bottleneck resources to feed the bottleneck exactly what it needs, when it needs it. |
The third step is to subordinate everything else to the bottleneck. Non-bottleneck resources should not produce more than the bottleneck can consume. Producing excess work-in-progress only creates inventory and hides problems. The ERP can enforce this by releasing work orders to non-bottleneck resources only when the bottleneck is ready to process them. This is called drum-buffer-rope in TOC language - the bottleneck sets the drumbeat, the buffer protects the bottleneck from variability, and the rope ties the release of new work to the bottleneck's pace. |
The fourth step is to elevate the bottleneck. Elevation means increasing capacity - adding a second shift, buying another machine, outsourcing some work, or improving the process. The ERP helps by quantifying the benefit of elevation. If the bottleneck is limiting output to one thousand units per week, and each unit generates one hundred dollars of profit, then increasing bottleneck capacity by ten percent adds ten thousand dollars of profit per week. This calculation justifies the investment. The ERP also tracks the results of elevation, showing whether the bottleneck moved or whether a new bottleneck appeared. |
|
6.5 Visualizing Load and Capacity - The Load Profile |
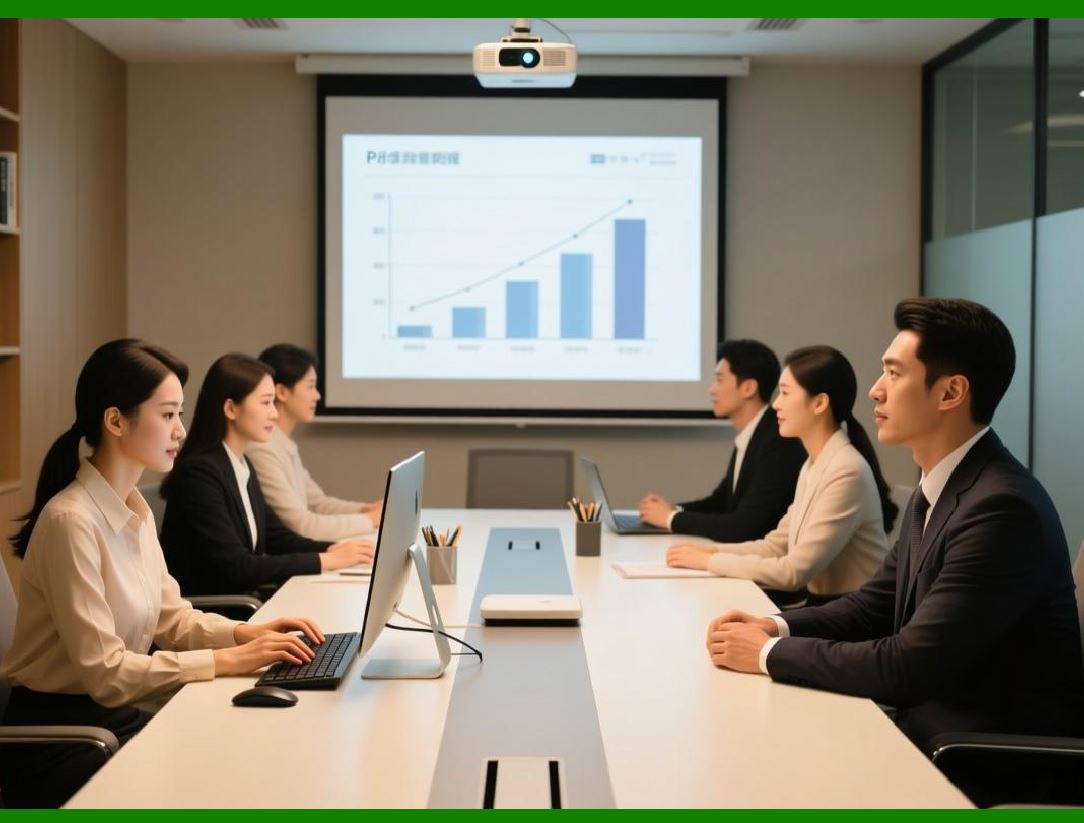
One of the most useful features of an ERP capacity planning module is the load profile - a visual chart that shows load and capacity on the same graph, over time. The load profile typically shows weeks on the horizontal axis and hours on the vertical axis. A horizontal line shows the available capacity. Bars or a line show the scheduled load. When the load bar rises above the capacity line, the planner sees an overload. When the load bar falls far below the capacity line, the planner sees underutilization. |
The load profile is not just a picture. It is interactive in modern ERP systems. The planner can click on an overloaded week and see which orders are causing the overload. They can drag an order from an overloaded week to a later week, and the system immediately updates the load profile, showing whether the overload is resolved. They can split an order across multiple weeks, or move a portion of an order to a different machine if an alternative routing exists. Each action has a cost - moving an order later may delay the customer promise, and moving to an alternative machine may increase setup time or reduce quality. The ERP can estimate these costs, helping the planner make trade-offs. |
The load profile reveals patterns that are invisible in tabular data. A factory might have no individual week with an overload, but every week is at ninety-five percent of capacity. That factory is running too lean. Any disruption - a machine breakdown, a quality problem, a supplier delay - will cause a cascade of late orders. The load profile shows this vulnerability. The planner can respond by reducing the MPS, adding capacity, or building inventory during calmer periods. |
Conversely, a load profile might show a pattern of peaks and valleys. The factory is overloaded for two weeks, then underloaded for two weeks. This pattern suggests that the MPS is lumpy. The factory might benefit from leveling - spreading the production more evenly across weeks, even if that means building some inventory during the valleys to serve the peaks. |
|
6.6 Finite Loading Versus Infinite Loading |
Traditional MRP and CRP use infinite loading. They assume that a work center can handle any amount of work, regardless of its capacity. The schedule is calculated without regard to overloads. Then the planner reviews the load profile and manually resolves the overloads. This is the most common approach in mechanical manufacturing, because it is simple and fast. |
An alternative is finite loading. Finite loading treats capacity as a hard constraint. The scheduling algorithm never assigns more work to a work center than its available capacity. When capacity is exhausted, jobs are pushed to later dates. Finite loading produces a schedule that is immediately feasible - no overloads exist. However, finite loading can be computationally intensive, especially for factories with hundreds of work centers and thousands of jobs. It also assumes that the planner can control the exact start and end times of every operation, which is rarely true on a busy shop floor. |
Most ERP systems offer both options. For rough-cut planning, infinite loading with manual overload resolution is usually sufficient. For detailed short-term scheduling of a bottleneck work center, finite loading can be very effective. A common hybrid approach is to use infinite loading for most work centers and finite loading for the bottleneck. The bottleneck schedule is frozen, and the non-bottleneck resources are scheduled around it. This combines the simplicity of infinite loading with the realism of finite loading exactly where it matters most. |
|
6.7 The Impact of Setup Times and Batch Sizes |
Capacity planning becomes much more complex when you consider setup times. A CNC machining center might take thirty minutes to change from one part to another. If you run ten jobs of ten parts each, you have ten setups - five hours of setup time. If you combine those ten jobs into one batch of one hundred parts, you have one setup - thirty minutes. The capacity required for the same total quantity can be dramatically different depending on how you batch the work. |
ERP capacity planning modules handle this by using the routing information. Each operation in the routing has a setup time (per batch) and a run time (per unit). When the system calculates the load for a work order, it multiplies the run time by the quantity and adds the setup time once. The system also respects minimum batch sizes. If a process is more efficient with larger batches, the planner can define a batch size rule. The ERP will then combine multiple requirements into a single batch when it makes economic sense. |
But batch sizes are not purely technical. They are also political. Larger batches reduce setup time and increase capacity, but they increase work-in-progress inventory and increase the time between when a part is started and when it is finished. This longer cycle time makes the factory less responsive to changes. The ERP can show the trade-off. It can calculate the capacity impact of reducing batch sizes - more setups, less available time for production. And it can calculate the inventory impact of increasing batch sizes - more work-in-progress, higher carrying costs. The planner chooses the balance that fits the factory's strategy. |
|
6.8 The Role of Overtime and Subcontracting |
When load exceeds capacity, the planner has two classic levers: add more time or move work outside. Adding more time means overtime, extra shifts, or weekend work. Moving work outside means subcontracting to another factory. |
Overtime is expensive. Workers typically earn one and a half times their regular rate for overtime hours. Machines run during overtime still consume energy and incur wear. But overtime is quick to implement and easy to reverse. For a temporary overload of a week or two, overtime is often the best answer. |
Subcontracting is also expensive, but for different reasons. The subcontractor adds their own markup, plus transportation costs. Quality may be less consistent than in-house production. Lead times may be longer. However, subcontracting can handle larger and longer-lasting overloads without burning out the workforce. It can also provide access to capabilities the factory does not have in-house, such as specialized heat treatment or exotic coatings. |
The ERP helps the planner choose between these options by tracking the costs. The system knows the standard labor rate, the overtime premium, and the subcontractor's price. When the planner faces an overload, the ERP can estimate the cost of resolving it with overtime versus subcontracting. The planner can also use what-if scenarios to compare strategies. What if we add ten hours of overtime on the bottleneck for the next three weeksWhat if we subcontract fifty percent of the work to an approved vendorThe ERP shows the cost and the resulting load profile for each scenario. |
|
6.9 The Moving Bottleneck - A Dynamic Challenge |
In a perfect world, the bottleneck would be fixed and stable. The factory would identify it, exploit it, subordinate to it, and elevate it. Then a new bottleneck would appear, and the cycle would repeat. In reality, bottlenecks can move unpredictably. A machine that is not a bottleneck for product A might become a bottleneck for product B. A supplier delay might turn a non-critical work center into a bottleneck overnight. |
The ERP helps manage moving bottlenecks by providing real-time visibility. Dashboards show the current utilization of every work center, color-coded from green (underutilized) to red (overloaded). A planner can see at a glance where the current constraints are. When a bottleneck moves, the planner can adjust the schedule accordingly. The ERP also tracks historical bottleneck data. Over time, patterns emerge. Perhaps a particular work center becomes a bottleneck every time a certain customer orders a certain product. The factory can prepare by building inventory of that product in advance, or by pre-positioning additional capacity. |
Some advanced ERP systems use bottleneck detection algorithms. These algorithms analyze the flow of work orders through the factory and identify the resources that are most frequently the limiting factor. The output is a ranked list of bottlenecks, with estimates of how much each bottleneck constrains total output. This data guides capital investment decisions. If the algorithm shows that the grinding department is the bottleneck for sixty percent of all orders, buying another grinder is a high-return investment. |
|
6.10 The Human Side of Capacity Planning |
Capacity planning is often the most politically charged activity in a factory. The planner who reports that the machining center is overloaded may be telling the manager of that center that they are not productive enough. The salesperson who hears that capacity limits prevent accepting a new order may accuse the planner of being too conservative. The finance manager who sees the cost of overtime may demand that the planner find a cheaper solution. |
The ERP cannot resolve these political tensions. But it can provide a neutral, fact-based foundation for the discussion. When the planner says the machining center is overloaded, they can show the load profile - actual scheduled hours versus actual capacity. When sales wants to accept an order that would overload the bottleneck, the planner can show the impact on existing orders. Which orders would be delayedWhich customers would be affectedThe data depersonalizes the conflict. It is not the planner versus sales. It is the reality of capacity versus the desire for revenue. |
Successful factories build a culture where capacity data is respected. The S&OP meeting, which we discussed in Chapter 4, is the forum where capacity decisions are made. Sales presents demand. Production presents capacity. The team works together to resolve mismatches. The ERP provides the data. The humans provide the wisdom and the courage to make hard choices. |
|
6.11 Real-World Example: The Gear Manufacturer's Bottleneck Breakthrough |
Consider a manufacturer of precision gears for industrial transmissions. The factory had a clear bottleneck: a gear hobbing machine that was forty years old but still produced the most accurate gears. The machine ran two shifts per day, five days per week. The load on the hobbing machine consistently exceeded capacity by about fifteen percent. The result was that gear orders were always late. The rest of the factory - the heat treat, the grinding, the inspection - often sat idle, waiting for gears from the hobber. |
The company implemented an ERP with robust capacity planning. The first step was to create accurate routings for every gear type, including setup times and run times on the hobber. The load profile confirmed what everyone already knew: the hobber was the bottleneck, overloaded by fifteen percent. |
The team applied the Theory of Constraints. First, they exploited the bottleneck. They analyzed every minute of the hobber's time. They discovered that the machine was idle for thirty minutes every shift during shift change, because the operator left early and the next operator arrived late. They staggered the shifts, eliminating the gap. They also found that setups were taking longer than the standard times. They created a setup checklist and trained all operators. Setup time dropped by twenty percent. |
Second, they subordinated everything to the bottleneck. The ERP was configured to release work to upstream processes only when the hobber was ready for it. This reduced work-in-progress in front of the hobber from three weeks to three days. The operators could now see exactly what to run next, without digging through a pile of partially completed orders. |
Third, they elevated the bottleneck. Based on the ERP's data showing that the hobber was the constraint for eighty percent of orders, management approved the purchase of a new, faster hobbing machine. The ERP's what-if analysis predicted that the new machine would increase total factory output by twenty-five percent. The actual result, after installation, was a twenty-eight percent increase. |
The bottleneck did not disappear. It moved to the grinding department. But the new bottleneck was less severe, and the factory's overall output was much higher. The capacity planning discipline, embedded in the ERP, became a permanent part of the company's operations. Every month, they reviewed the load profiles, identified the current bottleneck, and applied the cycle of exploit, subordinate, and elevate. |
|
6.12 The Difference Between Utilization and Effectiveness |
A common mistake in capacity planning is to focus too much on utilization. Utilization is the percentage of time a resource is busy. A machine with ninety-five percent utilization sounds efficient. But high utilization is often a warning sign, not a badge of honor. |
When a resource is highly utilized, it has little slack to absorb variability. A small delay in a raw material shipment, a minor quality problem, or a brief machine breakdown will cause the resource to fall behind. The backlog grows. Lead times stretch. The factory becomes brittle. |
The goal is not maximum utilization. The goal is effectiveness - producing the right products, at the right quality, at the right time, with minimal waste. Sometimes effectiveness requires keeping utilization lower than maximum, so that the factory has the flexibility to adapt to surprises. |
The ERP's capacity planning tools can help find the right utilization target. By simulating different levels of capacity, the planner can see the trade-off. Lower utilization means more slack, but also higher cost per unit because fixed costs are spread over fewer units. Higher utilization means lower cost per unit, but higher risk of delays. The optimal point depends on the factory's market, its customers' tolerance for lateness, and its cost structure. The ERP does not calculate the optimum automatically, but it provides the data for an informed management decision. |
|
6.13 Summary: From Reactive Firefighting to Proactive Balance |
Capacity vs. load is a simple concept. But in a busy mechanical factory, with dozens of machines, hundreds of orders, and constant disruptions, that simple concept becomes incredibly complex to manage. Without an ERP, capacity planning is reactive. Problems are discovered when they have already caused delays. The planner spends their time firefighting - expediting orders, shifting priorities, and apologizing to customers. |
With an ERP, capacity planning becomes proactive. The system shows the planner where overloads will occur, weeks before they happen. The planner can act - adding overtime, subcontracting, moving orders, or leveling the schedule - before any customer promise is broken. The bottleneck becomes visible, manageable, and eventually, elevatable. |
The Theory of Constraints provides the strategic framework. The ERP provides the tactical tools: load profiles, what-if scenarios, bottleneck detection, and integration with scheduling. Together, they turn capacity planning from a necessary evil into a competitive advantage. A factory that understands its bottlenecks and manages them deliberately will always outperform a factory that stumbles from one crisis to the next. |
In the next chapter, we will move from planning to execution. We will look at how the ERP controls the shop floor, tracking work in real time and closing the loop between the plan and the actual. But remember: shop floor control is only as good as the capacity plan that guides it. A plan that respects capacity is a plan that can be executed. And execution is where value is finally created. |
|
Key takeaways from Chapter 6: |
1. The bottleneck is the resource that limits total factory output - everything else should be subordinated to it. |
2. Capacity planning is not optional; ignoring capacity leads to expediting, chaos, and late deliveries. |
3. Rough-Cut Capacity Planning (RCCP) checks the MPS against bottleneck resources at a high level, while Capacity Requirements Planning (CRP) provides detailed, order-level analysis. |
4. The Theory of Constraints provides a five-step framework: identify, exploit, subordinate, elevate, repeat. |
5. Load profiles visualize the balance between load and capacity, helping planners see overloads and underutilization at a glance. |
6. Finite loading treats capacity as a hard constraint; infinite loading with manual resolution is more common, with finite loading reserved for bottlenecks. |
7. Setup times and batch sizes have a major impact on capacity - larger batches reduce setups but increase inventory and cycle time. |
8. Overtime and subcontracting are the two classic levers for resolving overloads; the ERP helps compare their costs. |
9. Bottlenecks can move; the ERP provides real-time visibility and historical analysis to track shifting constraints. |
10. High utilization is not always good - slack is needed to absorb variability and keep the factory robust. |
11. Real-world success requires both the ERP's tools and the organization's discipline to act on the data. |
 cs@easiersoft.com